Hey there, it’s Jake from your go-to deep groove ball bearing supplier—you know, the one who’s not just here to ship parts but to help you get this stuff right, no matter what. Today we’re talking about something that trips up a lot of folks: internal clearance in deep groove ball bearings. You’ve probably heard “internal clearance” thrown around, maybe even ignored it, but skip measuring it? That’s how you end up with noisy machines, overheated bearings, or worse—total breakdowns when you least expect it. I’ve seen it happen way too many times, so let’s break this down like we would over a coffee, no stuffy lab jargon that makes your eyes glaze over. Deep Groove Ball Bearings
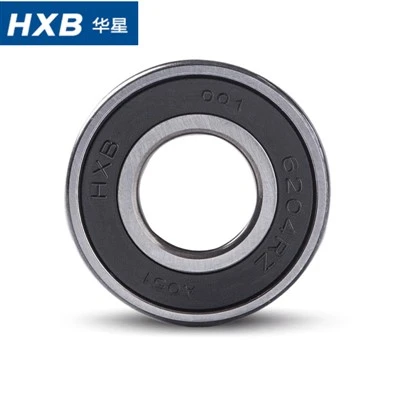
First, let’s get on the same page about what internal clearance actually is, because I don’t want anyone mixing this up with “play” or “gap” (though they’re related). Think of a deep groove ball bearing as three main parts: the outer ring, inner ring, and those little balls rolling between ’em. Internal clearance is the amount the inner ring can move—side-to-side or along the axis—inside the outer ring when there’s no load on the bearing, right? It’s not a one-size-fits-all number, either. If you’re running a conveyor belt that’s hauling heavy lumber, you need different clearance than if you’re spinning a dental drill that’s moving at 50k RPM. Too tight, and the bearing can’t expand when it heats up—boom, overheating, seizing, game over. Too loose, and you get wobble, vibration, and those annoying noises that make your customers call you at 2 a.m.
Now, the good stuff: how do we actually measure this? I’ve used a bunch of methods over the years, some basic, some for when you need pinpoint accuracy, and I’ll walk you through the ones we trust here at the shop. Let’s start with the easiest one—you can do this in a warehouse with a screwdriver and a dial indicator, no fancy lab gear required. That’s the radial clearance method, and it’s the most common because that’s how most bearings carry load.
Here’s how it works step by step. First, you gotta set the bearing up right—this isn’t like measuring a bolt, you need it stable. Take the bearing, put it on a flat surface (a workbench, or even the top of a pallet if you’re in a pinch), and make sure the outer ring is sitting dead level so it doesn’t rock. Next, stick the dial indicator on the outer ring—wait, no, wait: actually, the inner ring is what we’re moving here, right? Wait, let me correct that for you. If you’re measuring radial clearance, you clamp the inner ring in place first—use a vise, just don’t squeeze it so hard you deform the ring, that’ll mess up your readings. Then, rest the dial indicator’s plunger on the top of the outer ring, make sure it’s zeroed out. Now, push the outer ring straight down as far as it will go, then pull it straight up as far as it will go. The difference between those two numbers on the dial is your radial internal clearance. Yeah, that’s it. I do this all the time when I’m testing a batch before it ships—quick, takes less than a minute, and gives me a baseline. But pro tip: turn the bearing a quarter turn and do it again. If the number jumps around, there’s probably a defect in the bearing, like a ball that’s too big or a groove that’s off. That’s why we do repeat checks, not just one.
But wait, that’s radial—what if you need axial clearance? That’s the side-to-side movement along the bearing’s center line, and that’s super important for things like pumps or motors where there’s thrust load. The method here is almost the same, just oriented differently. Clamp the inner ring again to keep it steady, stick the dial indicator on the end face of the outer ring (or if you’re doing it on the inner, clamp the outer ring this time, whatever works). Then push the outer ring all the way to one side, zero the dial, then push it all the way to the other. The difference is your axial clearance. This one’s trickier because you have to make sure you’re only moving it along the axis, not twisting it—twist it, and you’re getting a fake high number, which is useless. I usually use a small pry bar for this, gentle pressure, not yanking, that’s how I avoid twisting.
Now, if you’re working in a quality control lab, or you need super precise numbers because you’re making like medical devices or aerospace parts, we use a more specialized tool: a clearance measuring machine. These aren’t something you keep in your back pocket, but if you’re ordering 10k bearings a month, it’s worth having one on site. These machines apply a consistent, light load (usually like 10% of the bearing’s dynamic load rating) so you’re not just measuring slack, you’re measuring actual working clearance. They hook up to a computer and spit out a exact number, not a dial reading, and even tell you if it’s within the ABEC or ISO tolerance class you ordered. Speaking of tolerance classes—don’t sleep on those. We ship our deep groove ball bearings in standard clearance (C0) for general use, but if you need C3 for high temps or heavy loads, or C2 for low vibration, you gotta specify that when you order, and the machine will check to make sure it hits that mark.
Wait, let’s talk about common mistakes everyone makes, including me when I was new at this. First, not accounting for mounting. Oh man, that’s a big one. The clearance you measure off the shelf is static clearance, but once you press that bearing into a housing or onto a shaft, that changes. If you press the inner ring onto a shaft that’s too tight, the inner ring expands, which reduces clearance—could be 20% less, even more. Same with pressing the outer ring into a housing that’s a squeeze fit: outer ring expands, reduces clearance. So if you’re measuring after mounting, you have to do it while it’s in the assembly, not just off the bearing alone. I had a customer a year ago who ordered C3 bearings, measured them on the shelf, thought they were too loose, sent ’em back—turns out when they pressed ’em into the pump housing, the clearance dropped right into C3. Oops. Don’t be that guy.
Another mistake: not checking every bearing. Yeah, sometimes a batch will have one bad one, and if you skip checking, that bad one ruins your whole machine. We do a 100% check on all our custom clearance orders, and a random sample (like 5% of a batch) on standard, because we don’t want to send out something that makes us look bad. And don’t forget about wear. If you’re measuring a bearing that’s already been running, clearance will be higher— that’s a sign it’s worn out, need to replace it before it fails. I had a customer’s conveyor stop mid-shift last month, we came out, measured the bearings, clearance was way over the limit, they had to shut down for 3 days. Lesson learned: periodic checks, not just when it breaks.
Wait, should you use a feeler gauge? I get asked this a lot. Some old-school guys swear by sticking a feeler between the ring and a ball to measure, but here’s the thing: that’s super inaccurate. The ball is a sphere, so the feeler’s gonna slip, and you’re only measuring one point, not the whole circumference. I tried this once on a rush order, it was a mess, the numbers were all over the place. The dial indicator method is way more consistent, even for small bearings. Save the feeler gauge for checking spark plugs, not bearing clearance.
Let’s also cover when you need what type of clearance, because that’s half the battle. Standard C0 is for most general stuff: fans, small pumps, light conveyor rollers. If your bearing’s gonna run over 100°C, or have heavy radial loads, or both, go for C3. C2 is for low-noise applications, like appliances or office equipment, where wobble would be noticeable. And if you’re working in extreme cold, wait—cold makes materials contract, so you might need even higher clearance than C3, because when the bearing gets cold, clearance drops, could seize. That’s something we help customers with all the time, picking the right clearance so they don’t have to worry.
Now, let’s tie this back to why this matters for you, the customer. I’m not here to sell you bearings that are just cheap— I’m here to sell you bearings that work for your application, because if your machine breaks, I lose a customer. So when you’re checking clearance, whether you’re doing it in your shop or receiving a bearing from us, make sure you note two things: what you measured, and what the spec should be. If you’re not sure what spec you need, shoot me an email or give us a call—we’ve got engineers on staff who can help you figure it out, no sales pitch, just straight advice.
Wait, let’s recap real quick so you don’t forget. First, know what you’re measuring: radial for most loads, axial for thrust. Use the dial indicator method—it’s easy, accurate, no fancy tools. Don’t forget that mounting changes clearance, so measure after you put it together. Avoid feeler gauges, they’re garbage for this. Pick the right clearance class for your job, not just the cheapest. And if something doesn’t look right, don’t guess—reach out.
I’ve been doing this for 12 years, working with deep groove ball bearings, and I’ve learned that the little stuff, like checking clearance, is what separates a bearing that lasts 2 years from one that lasts 10. I’ve seen customers save thousands by just doing a quick check every month, and I’ve seen thousands lost because they skipped it. At the end of the day, bearings don’t have to be rocket science, but taking 5 minutes to measure clearance can save you a ton of headaches.
If you’re ordering bearings from us, every single one we ship comes with a test report that has the clearance measurement we did before it left our shop, so you don’t have to second-guess it. But if you need help measuring, or you’re not sure what clearance class you need, or you just want to chat about your bearing problems, hit us up—we’re here to help, not just take your money. No stuffy phone calls, no auto-replies, just real people who know this stuff.
Don’t let bad clearance ruin your next project. Grab your dial indicator, follow these steps, and you’ll be good to go. And if you’re in the market for new deep groove ball bearings, or you just need to confirm your current ones are up to snuff, reach out to our team. We’ll get you sorted, no hassle.
Angular Contact Ball Bearings References
- American Bearings Manufacturers Association (ABMA). ABMA Standard 20: Clearance for Rolling Bearings. 2020.
- International Organization for Standardization (ISO). ISO 1132-1: Rolling bearings – Tolerances – Part 1: Dimensions, deviations and designation system. 2019.
- Jones, A.B. Rolling Bearing Analysis. 5th ed. Wiley, 2007.
Hangzhou Huaxing Kechuang Holding Group Co., Ltd.
Hangzhou Huaxing Kechuang Holding Group Co., Ltd. is one of the leading manufacturers and suppliers of deep groove ball bearings in China, featured by quality products and good service. Please rest assured to buy bulk durable deep groove ball bearings from our factory. Welcome to view our website for more information.
Address: No.553 Yingbin Road, Linping, Hangzhou, 311100, China
E-mail: wmb@huaxingbearing.com
WebSite: https://www.hxbbearing.com/
